Core Capabilities
The Capabilities Backing Every CELINA Product
At CELINA, we focus on engineering expertise, manufacturing excellence, and customer commitment. We support every product, project, and partnership with those three core capabilities. Enabling us to easily cross serve military, industrial, and commercial customers.
Expertise That Works Together
Behind every successful project is a foundation of proven capabilities.
Our teams work together to understand customer requirements, transforming them into dependable solutions. We take the same care with a single commercial tent as we do with a complex government order. Our goal is to deliver exceptional results through disciplined execution.
Core Capabilities
What CELINA Does Best
Explore where our capabilities create value, and review the proof behind our work.
Engineering
Our engineering team brings technical expertise to real-world applications. For every product, our engineers must balance manufacturing ease with performance and durability. The end goal is practical products built for demanding environments.
Product Development
At CELINA we invest in new tech, manufacturing processes, and product development. We use customer feedback to create better solutions. We work to continuously improve quality, efficiency, and product performance.
Quality Systems
CELINA’s quality management system is ISO 9001:2015 certified. We build quality into every stage of manufacturing by standardizing processes. Our products go through verification at every stage. That, in turn, supports consistent, quality products across industries.
Program Management
Our dedicated product management team handles every CELINA project. They work with customers, suppliers, and internal teams to ensure projects remain organized. Our team is responsive and keeps projects aligned from planning through delivery.
Customer Partnership
We work with customers to understand their needs. We work to meet any changes and to build long-term relationships based on trust. At CELINA, we understand that strong communication leads to shared success.
Organizational Scale
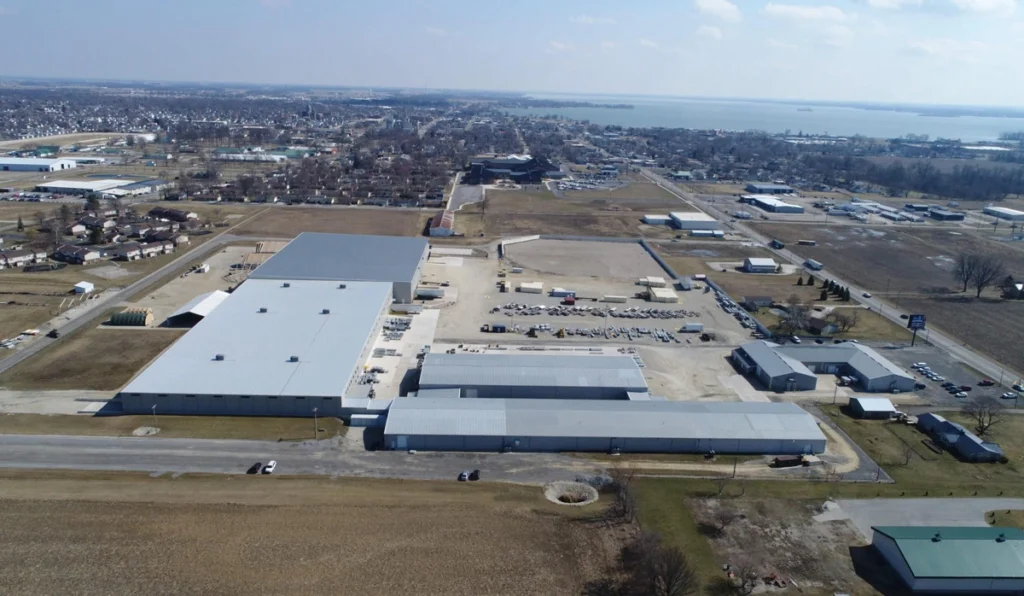
Behind every CELINA project is the resources of a corporate organization. Our facilities sit on a 58-acre campus. We operate more than 300K square feet of manufacturing, warehousing, and distribution facilities. CELINA has the capacity, resources, and flexibility to support projects of every size.
Our Footprint
Built to Every Customer
CELINA works from centralized headquarters in Celina, Ohio. The 58-acre campus brings together engineering, manufacturing, warehousing, distribution, and corporate operations. This allows for accelerated decision making and communication. It also supports consistency and quality during every stage of production.
Our facilities provide the space and capacity to support various projects. Be it commercial tent production, government programs, or custom printing and manufacturing. It also gives us the flexibility to adapt to your needs as they evolve.
Common Questions
CELINA Capabilities FAQ
What does CELINA’s engineering team support?
CELINA engineering supports product development, manufacturing, custom enhancements, and technical collaboration across projects.
Can CELINA manage large, multi-year programs?
Yes, CELINA supports large, multi-year projects. Most long-term projects are for our government, military, and industrial customers. We support these projects with dedicated program management services. And we ensure long-term customer support and precise manufacturing planning throughout. CELINA also handles small, one-off projects for commercial tent customers.
How does CELINA’s quality system work?
CELINA’s has an ISO 9001:2015 quality management system certification. We also standardize manufacturing processes, document procedures, and conduct regular inspections.
Where is CELINA’s manufacturing located?
CELINA’s primary manufacturing campus is in Celina, Ohio.
Tell Us About Your Project
Looking for tents, shelters, or engineered fabric manufacturing?
Let us know what you need. Start a conversation with our team.